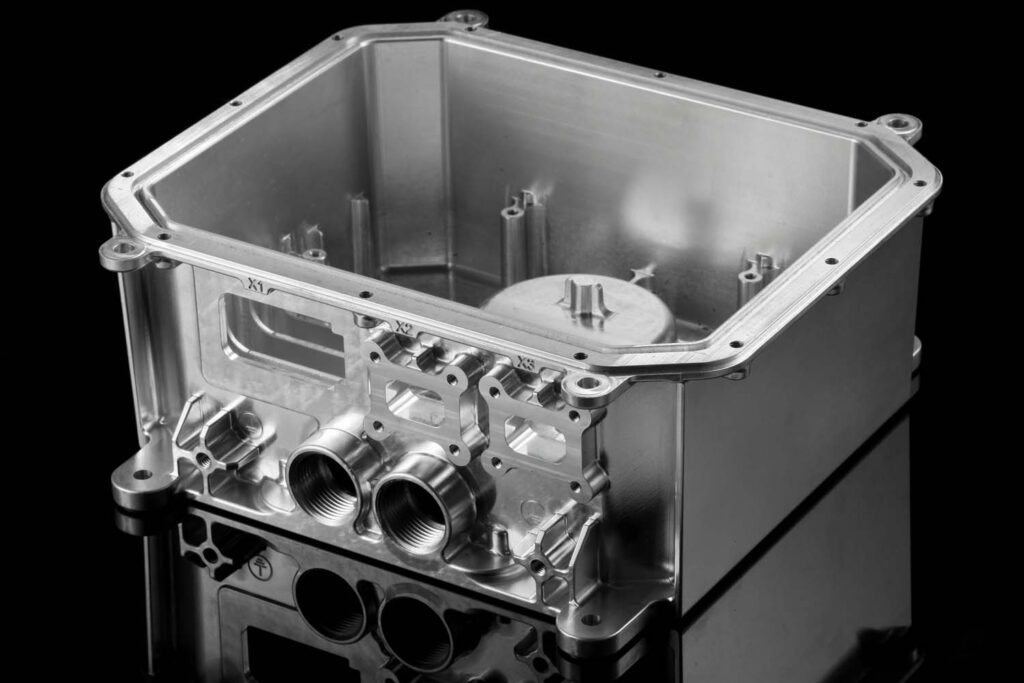
For aluminum CNC machining flatness, define the surface, acceptance condition and inspection arrangement before comparing quotations. A plate that appears flat while firmly clamped may behave differently after release. Purchasing teams therefore need a shared definition of whether acceptance applies in the free state or in a specified assembly fixture. Supply the alloy and temper, stock form, drawing revision, finishing requirement and intended mating arrangement. Ask BOLE to review manufacturability and the proposed inspection method against those inputs. Do not treat a general machining capability statement as a guaranteed flatness result for an unreviewed component.
Define the surface and the acceptance condition
Identify exactly which face controls assembly performance and which drawing requirement applies to it. Flatness and the relationship between two surfaces are different questions; avoid replacing a drawing review with the instruction “make both sides flat.” Show sealing tracks, thermal interfaces, mounting pads and areas interrupted by pockets. Specify whether the component is evaluated before or after finishing. Where assembly loading matters, provide the fixture drawing and loading sequence as a separate condition instead of leaving the inspector to infer them from a photograph.
Separate free-state behavior from fixture behavior
Record the agreed support locations, component orientation, measurement coverage and any restraint used during evaluation. Supporting a flexible part differently can change the observed result, while forceful restraint can conceal distortion that affects later assembly. Ask the supplier to explain how the proposed inspection arrangement represents the drawing requirement. If both released and installed behavior matter, request two clearly identified records. Do not combine them into a single unexplained pass mark. An assembly trial can provide useful evidence, but it should have its own acceptance basis.
Connect the quotation to material and geometry
Send the actual alloy, temper, stock dimensions and relevant material documentation requirements. Thin floors, long spans, deep pockets and uneven material removal deserve particular review because the final geometry may be sensitive to the manufacturing sequence. Ask what information the shop needs to assess those risks and whether the design should change before production. Do not prescribe an unverified universal machining sequence. The quotation should identify assumptions about stock, operations, handling and review samples so competing offers describe comparable work.
Review finishing before freezing the drawing
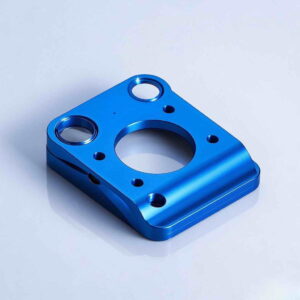
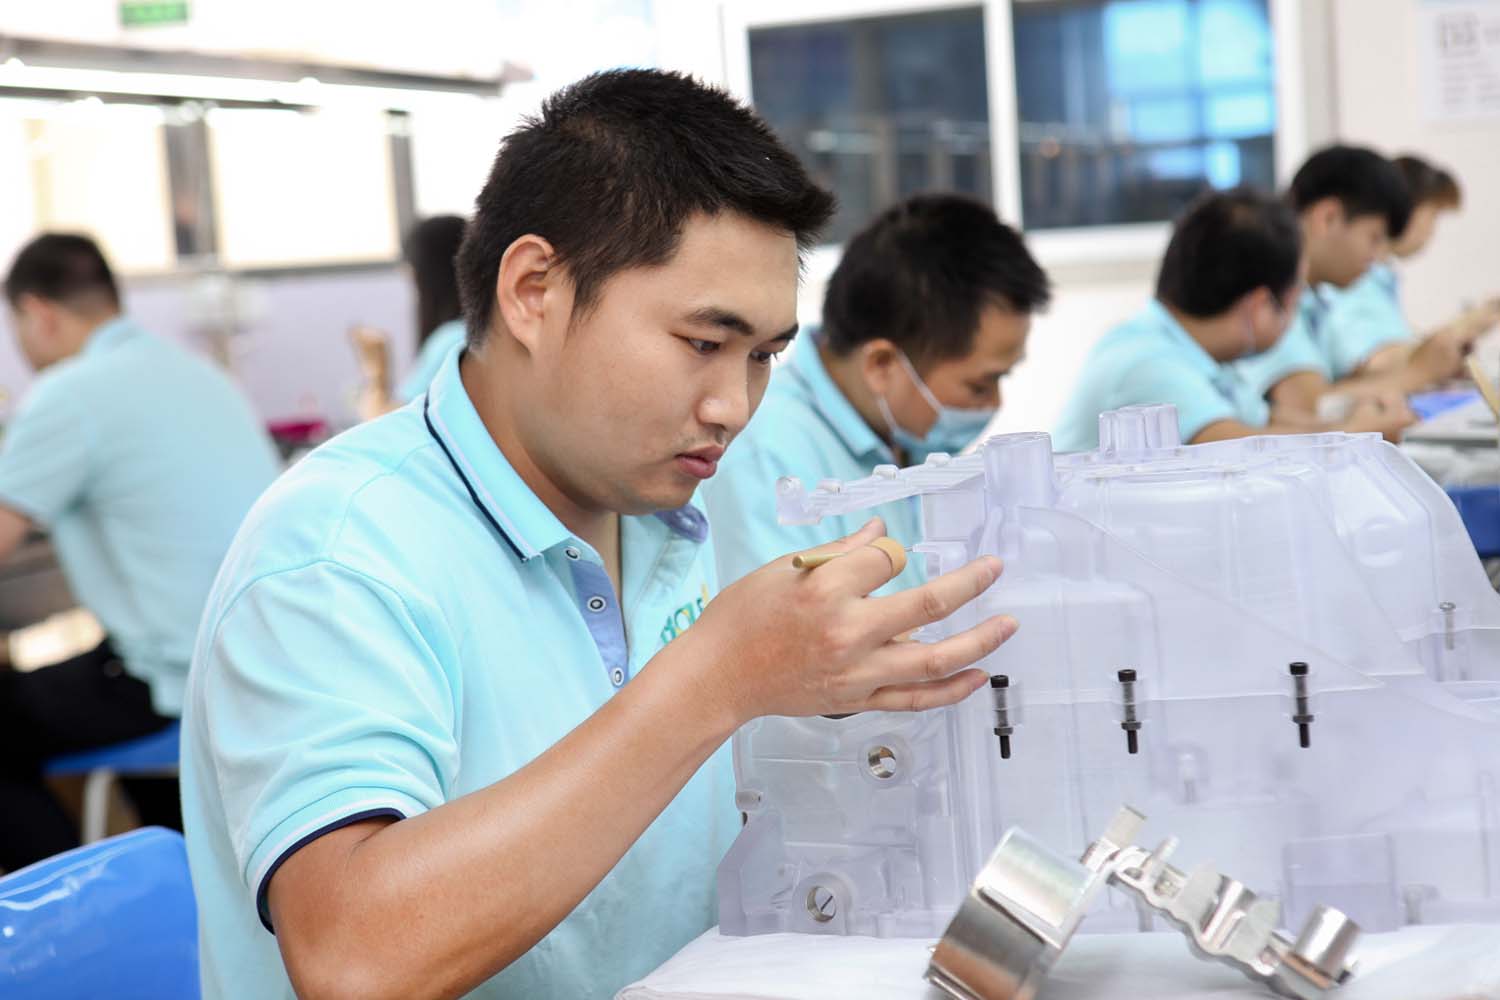
Mechanical finishing, anodizing and other specified treatments belong in the same drawing review as the machined surfaces. Identify masked interfaces, handling limits and the stage at which each dimension is accepted. The accompanying finishing photograph illustrates a separate operation; it does not establish a flatness tolerance or prove that a particular treatment preserves every geometry. Ask for confirmation of the proposed route, inspection stage and any dimensional allowance. If a finish changes after sample approval, review its implications before transferring the previous acceptance record to a new order.
Require an inspection record that another team can repeat
A useful record identifies the part and drawing revision, inspected face, support arrangement, equipment or method, inspection stage and result. Agree how observations relate to the specified requirement and what evidence will accompany the shipment. A summary stating only “CMM checked” leaves important questions unanswered. Discuss access to recessed faces and how the measurement arrangement will be qualified for the actual geometry. Confirm the scope and cost of first-article and production reporting instead of assuming that every quotation includes the same documentation.
Plan sampling, handling and repeat-order control
Approve a representative first article using the same drawing, material basis and finishing route intended for the order. Distinguish technical sample approval from permission to ship later batches without the agreed checks. Protective packing should prevent contact damage and avoid stressing a vulnerable face in transport. Retain accepted photographs, inspection records and authorized deviations. For repeat orders, confirm what happens when stock form, fixture, manufacturing sequence or finish changes. A traceable revision decision is more useful than an unsupported promise that the next batch will be identical.
Compare offers on the same acceptance basis
Ask each quotation to list the inspection condition, document package, sample scope and any excluded operation. Clarify whether the price includes fixtures, first-article review, finish coordination and protective packaging. Delivery timing and order quantity must be confirmed for the reviewed design; this article establishes neither a standard minimum quantity nor a guaranteed lead time. Close disagreements about acceptance before placing the production order. If the buyer changes the surface requirement later, request a revised feasibility and commercial review rather than relying on the original price.
Buyer selection and acceptance table
| Buyer need | Recommended product or scope | Key specification | Why it matters |
|---|---|---|---|
| Released flatness | CNC-machined aluminum part with agreed evaluation | Face, orientation and support | Separates geometry from clamping effects |
| Installed mating behavior | Reviewed part and assembly fixture | Loading sequence and interfaces | Makes the assembly review reproducible |
| Finished surface acceptance | Machining and confirmed finishing route | Inspection stage and masking | Prevents an ambiguous final-state requirement |
| Repeat production | Controlled drawing and inspection package | Revision and change notification | Preserves the approval basis |
Suitable and unsuitable purchasing scenarios
Best for OEM engineers and purchasing teams buying aluminum plates, housings or interfaces with a defined mating requirement. Suitable for prototype qualification and repeat-batch acceptance planning. Not suitable for approving a tolerance without drawings, using heavy clamping to disguise released distortion, or interpreting an illustrative product photograph as measurement evidence.
Frequently asked purchasing questions
Does a clamped measurement prove free-state flatness?
It establishes only the condition that was actually evaluated. Restraint can affect a flexible component, so record the support and clamping arrangement and relate it to the drawing requirement. If released behavior matters, agree how that condition will be checked. Retain separate results when both assembly behavior and a free-state requirement are part of the purchasing specification.
What should accompany a flatness RFQ?
Provide the controlled drawing, marked surfaces, alloy and temper, stock assumptions, quantity, finishing requirement and intended assembly. Explain whether acceptance is before finishing, after finishing or under a defined fixture condition. Include the document package and target delivery date. Ask the supplier to identify missing information and deviations before comparing the commercial quotation with another offer.
Can BOLE guarantee a tolerance from a product photograph?
A photograph can illustrate a component family, but it does not establish dimensions, material condition, measurement capability or manufacturing feasibility. Ask BOLE to review the actual drawing and acceptance plan before a commitment is made. The offered tolerance, inspection method, sample requirement and production scope need written confirmation for the particular geometry and quantity being purchased.
How should finishing be included in acceptance?
Identify the required finish and the stage at which each controlled surface is inspected. Show masking and protected interfaces on the drawing where relevant. Ask whether the proposed process route and dimensional allowances suit the design. Retain the accepted sample and report with the finish specification. A changed finish should trigger review of affected requirements before repeat production is approved.
Which records make a repeat order easier to review?
Keep the accepted drawing revision, material basis, first-article report, evaluation arrangement, finish requirement and packing instructions together. Record approved deviations and the person authorized to accept them. Ask how production lots will be linked to those records and how process changes are reported. This creates a reviewable order basis without claiming that a previous favorable sample guarantees every later batch.
Request a drawing-based manufacturing quotation
Review BOLE’s CNC machining services, then contact the team for a project quotation. Send the model or application, country, prototype and production quantities, controlled drawings or CAD files, material and key parameters. Include OEM labeling or packaging, required tests or certificates and the target delivery date. Ask the team to confirm the offered configuration, inspection scope, customization feasibility, minimum quantity and delivery proposal for the reviewed design. Identify unresolved requirements before authorizing production.
- Which face and acceptance condition control the assembly?
- What alloy, temper, quantity and drawing revision apply?
- Which finish, inspection documents and packaging need confirmation?
- What destination, required tests and delivery target should the quotation address?